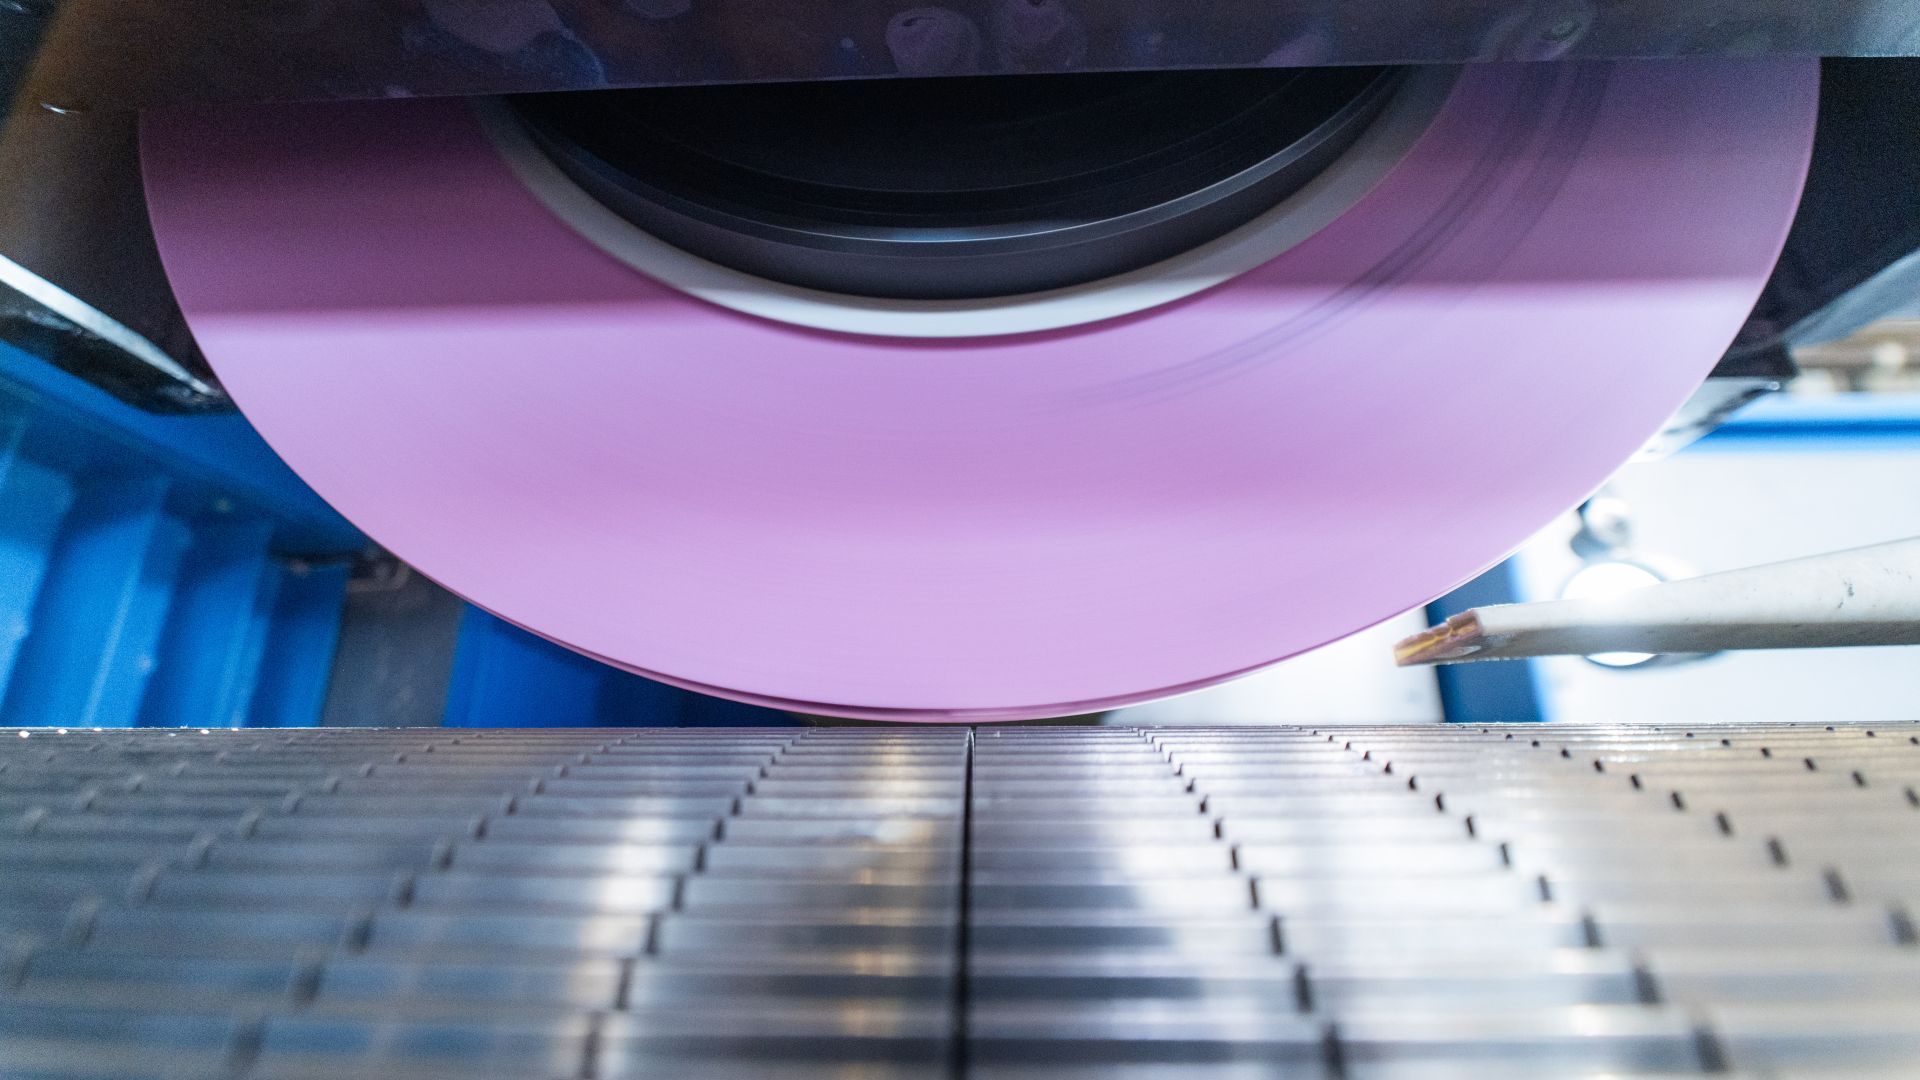
In regrinding, we first analyse the state of wear. This is followed by mechanical and technical processing, then recoating or adjustment, and finally the quality inspection. The regrinding and coating of corrugating rolls, pressure rolls and glue applicator rolls is explicitly included in the scope of our ISO 9001 certification.
What can be repaired is only decided after the inspection. Every scope is assessed individually and quoted separately. Some damage we can fully remedy, some we cannot, and we will tell you so.
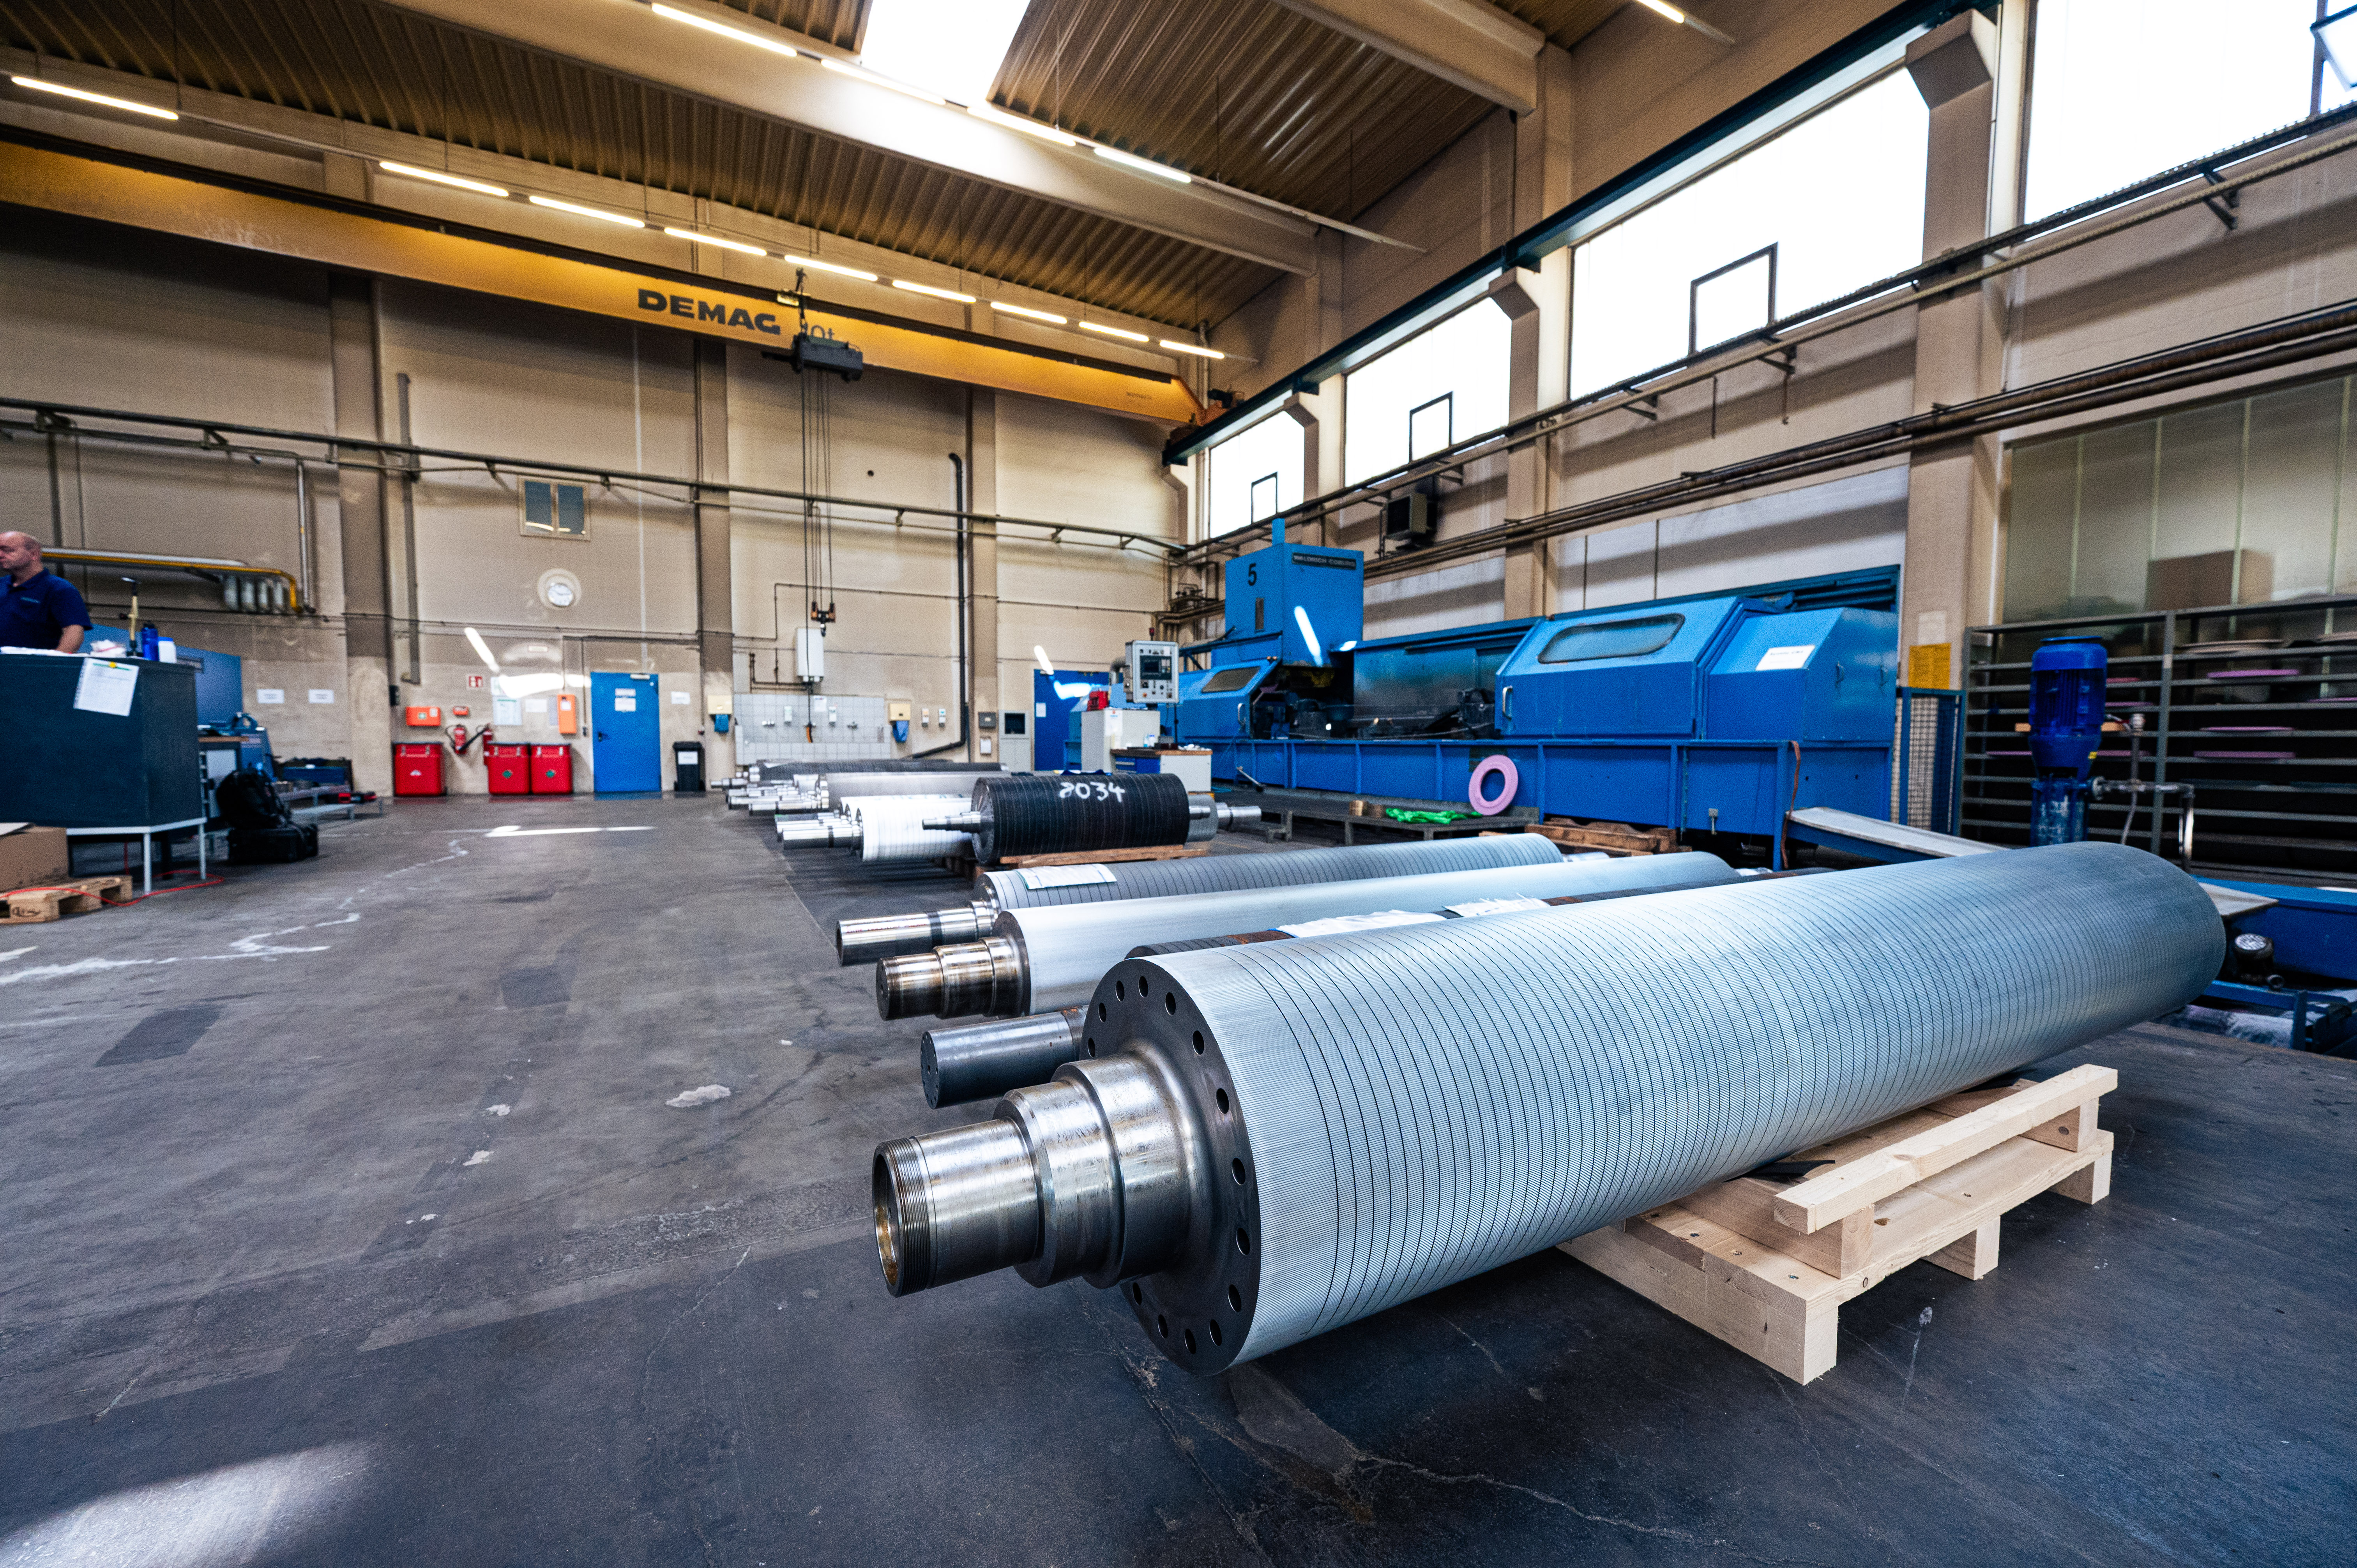
We repair broken flutes using special welding processes. For micro flutes with localised damage, we use laser welding because the heat input can be controlled. Laser welding in the flute roots also maximises the number of regrinds still possible later.
We rebuild damaged bearing seats to OEM dimensions using tungsten spraying. This restores the geometry and fit of the seat.
If bearing damage was detected too late and material and threaded areas have been worn away, we cannot offer a repair with guaranteed success. We will, however, show you alternatives.
When Viton or graphite seal rings stop working, the risk of bearing damage increases as the leak progresses. We machine off the damaged area and rebuild it with tungsten carbide spraying.
With extensive material loss, the scope of repair depends on the remaining base material and on the geometry. We define the repair concept after the inspection.
We rebuild surfaces with improved mechanical properties. The aim is to restore reliable process conditions.
Where thermal effects on the roll body need to be avoided, we use machining and cold welding.
We replace broken bolts, and we reseal or replace leaking journals. Both are quoted separately after the inspection.
If damage is too advanced to be repaired with guaranteed success, we do not offer the repair. Instead, you receive an assessment of the alternatives.
We have developed our own repair solutions for machines from certain manufacturers.
Pictures are enough for an initial assessment. They show us which direction makes sense before you ship the roll.
Before deciding on regrinding, the same questions usually come up. Here are the short answers.
Over the life of a set, we can usually achieve four regrinds instead of three, and in some cases even five. The inspection shows how many are still possible for your roll.
No. Every repair scope is only assessed after the detailed inspection and then quoted separately. For most damage patterns, that is the only reliable order.
Yes. The regrinding and coating of corrugating rolls, pressure rolls and glue applicator rolls is within the scope of certification to DIN EN ISO 9001:2015.
As a roll grinding specialist with our own coating plant, we cover corrugating roll grinding from start to finish: wear analysis, stripping, profile grinding, recoating and quality inspection under one roof in Föritztal. For us, regrinding rolls means more than removing material; it means restoring the geometry.