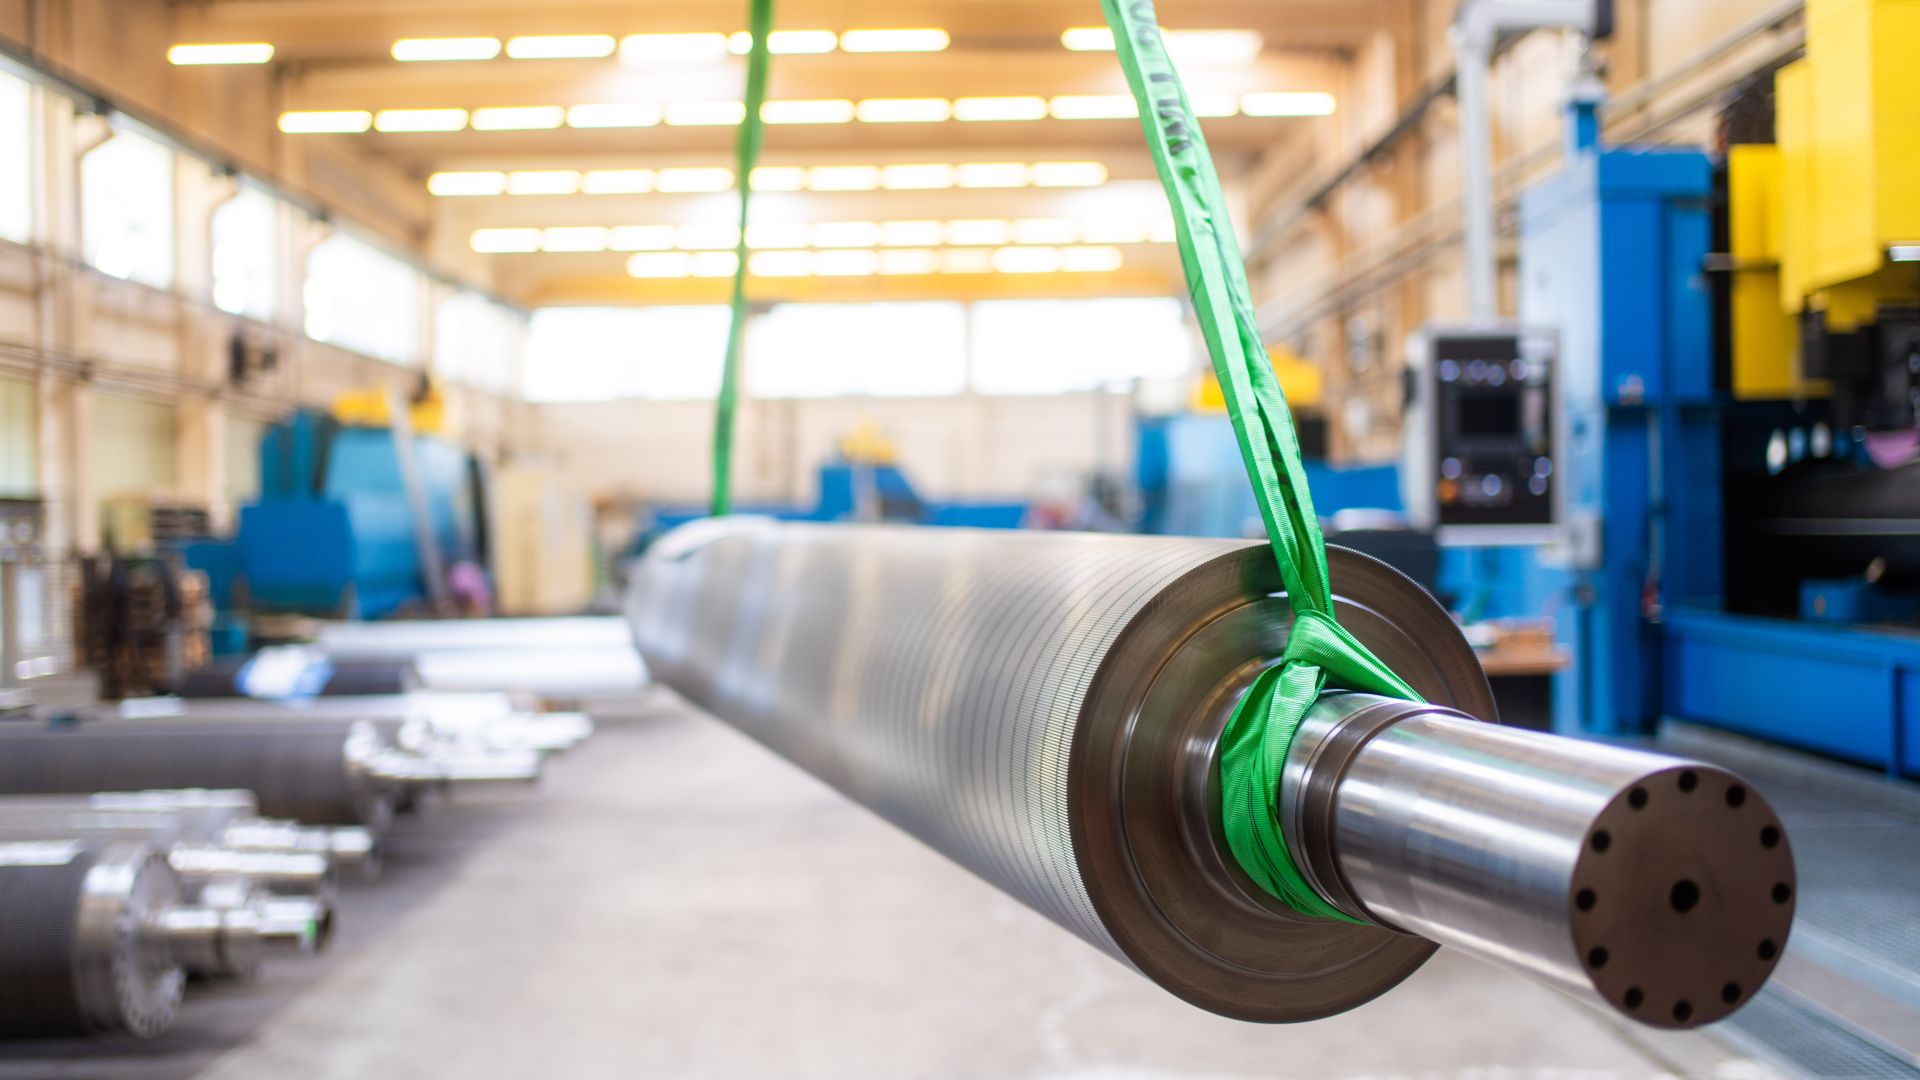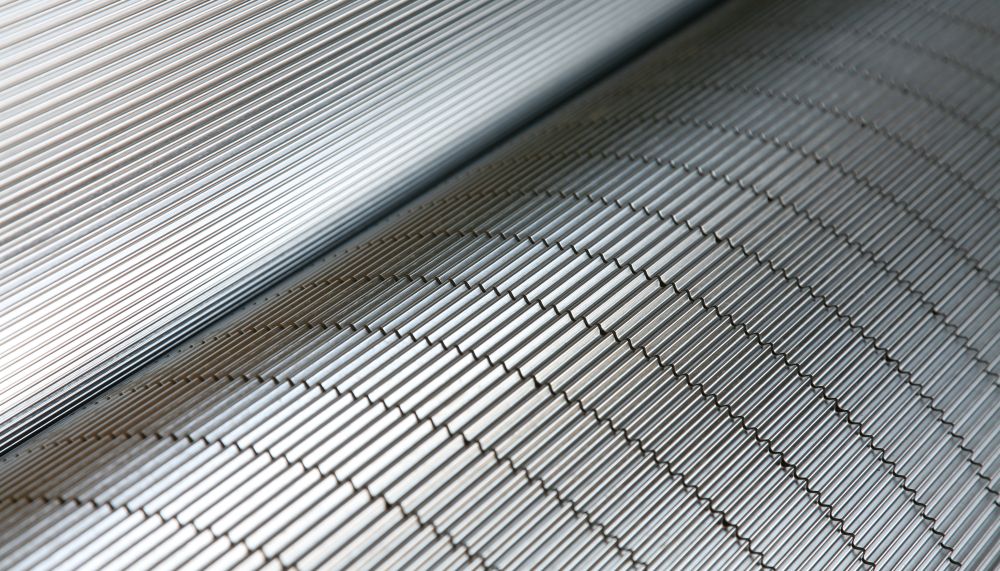
A corrugating roll turns flat paper into the flute that gives corrugated board its stiffness. In the single facer, two of them always work against each other: heated, under pressure and at high speed. Their geometry determines how much paper is consumed and how stable the finished board is. Their surface determines how long it stays that way. That is why the corrugating roll is the most heavily stressed component in the corrugator and the one with the clearest impact on cost efficiency.
Before we build a roll, we look at the existing one. In the PACE profile analysis, we compare your current profile with a proposal for a new one. At the same time, we check which coating suits the papers and the single facer actually running at your plant. You get the comparison and make the decision.
| Feature | Value |
|---|---|
| Concentricity | 20 µm |
| Flute profiles designed in our archive | 140,000, from 0.50 mm to 10.00 mm flute height |
| Known single facer types | 104 |
| Surface hardening | Induction or nitride hardening |
| Heating | Conventional, peripheral or Thermogrooves |
| Coating | Tungsten carbide (ROCKWELLE®), chrome |
| Application process | HVOF, high-velocity oxy-fuel spraying |
| Max. roll body dimensions | ø 620 × 3,000 mm |
| Max. weight | 3.5 t |
| Testing | DIN EN ISO 9001:2015 |
| Certificates | CE, ASME |
A corrugating roll costs money once when you buy it and continuously while it runs: a take-up factor that is too high, too much waste after downtime, poor heat transfer or too much vibration limiting speed. Over the life of a set, the purchase price is the smaller item. It is just the only one that appears on the quote.
Machine type, flute type, working width. That lets us assess what suits you, and we will get back to you with specific questions. If you have profile data or documents for your current roll, please attach them.
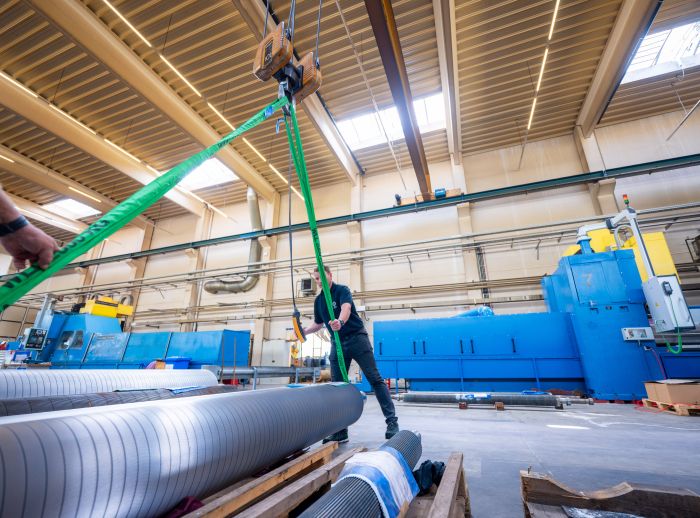
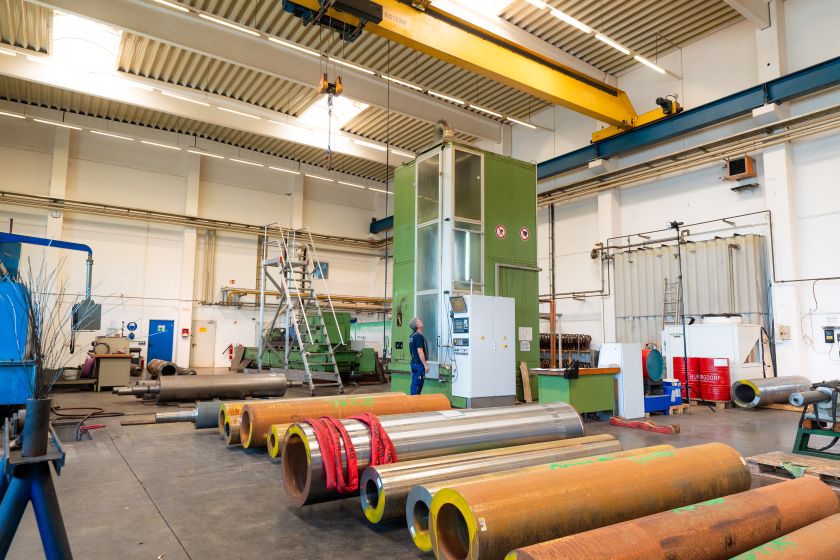
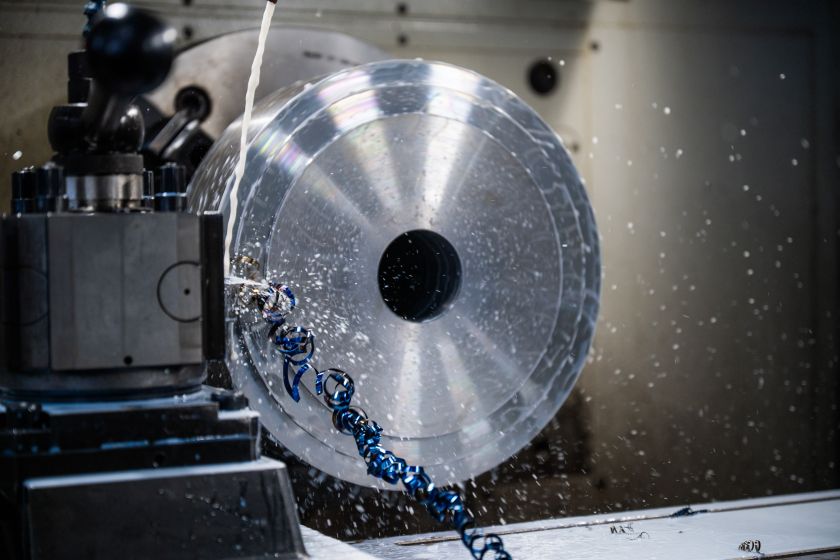
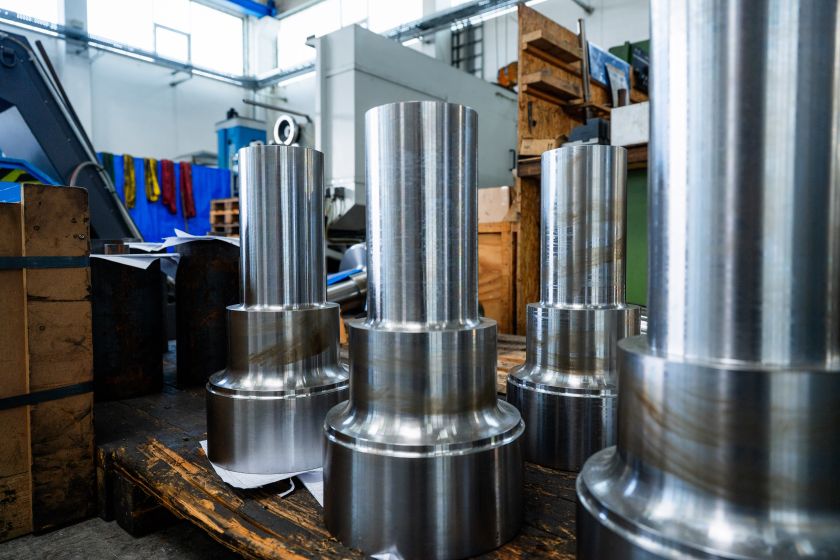
Most enquiries revolve around the same points: regrinds, special profiles and whether a new roll is needed at all. Here are the short answers. If your question is not among them, get in touch directly.
In the single facer of a corrugator, a corrugating roll turns flat paper into the fluted structure. Two heated rolls work against each other and emboss the profile that later gives the corrugated board its stiffness.
Over the life of a set, our rolls usually allow four, in some cases even five, regrinds instead of three. An inspection tells you how many are still possible on your roll.
Yes. We design the roll geometry individually to suit material, process and application. 140,000 documented flute profiles and 104 known single facer types form the basis for this.
Often, yes. If the roll body and bearing seats are in good condition, we regrind the profile and recoat it. After the inspection, we tell you what is possible.
As a German manufacturer of corrugating rolls, we supply corrugated board plants on every continent. Alongside corrugating rolls for single facers, we manufacture special rolls and industrial rolls for related applications, all with the same in-house production depth in Föritztal.